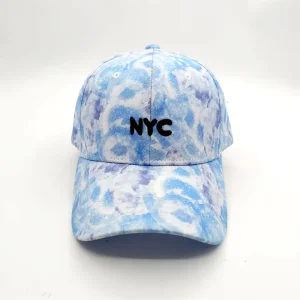
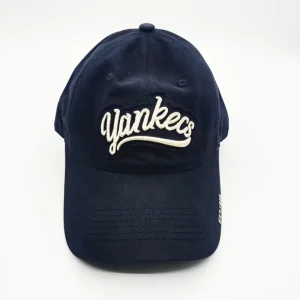
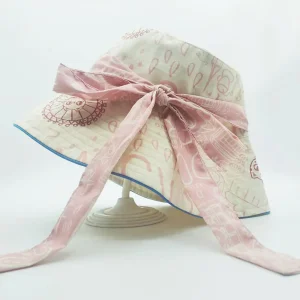
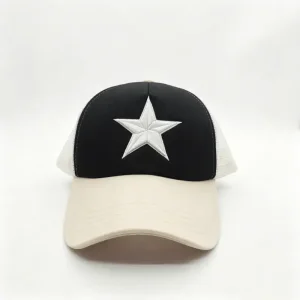
Engineered with lightweight, UV-reflective cotton twills, breathable mesh structures, and custom tactile detailing.
Uncovering the shift toward tech-enabled textiles, eco-compliance, and resilient supply chain consolidation in Qingdao's premier industrial cluster.
Situated in Ligezhuang Town, officially known as the "Hometown of Hats in China," Chenyou consolidates spinning, weaving, computerized dyeing, laser cutting, and blocking within a 15-kilometer radius to minimize turnaround latency and transport emissions.
By bypassing third-party trading intermediaries through vertically integrated in-house export infrastructure established in 2018, overseas DTC labels and retail enterprises secure 18–24% lower landed manufacturing costs while elevating raw spec transparency.
Deploying strict AQL 2.5 quality control thresholds, our facility embeds digital stitch-density tracking, mechanized steam blocking, and calibrated optical needle detection to safeguard international brand integrity before departure.
Combining traditional artisan millinery with advanced automated equipment to solve core thermal, ergonomics, and structural retention hurdles.
Summer hat engineering begins at the yarn level. We utilize high-density poplin weave, garment-dyed combed cotton, and technical RPET matrices rated UPF 50+ to block over 98% of harmful UVA and UVB radiation without suffocating breathability.
By combining laser-cut perimeter eyelets, ultrasonic punch channels, and multi-ply hydrophobic sweatband tapes, our hats rapidly pull sweat away from the temples, evaporating condensation within minutes during hot weather.
Utilizing high-memory, water-tolerant EVA visor cores and flexible poly-woven inserts, our summer bucket hats and baseball caps survive repetitive crushing, luggage packing, and machine washes without warping or breaking profile.
Rigorous environmental frameworks, third-party social audits, and friction-free logistics across key Western and APAC corridors.
BSCI-audited workshop facilities guaranteeing humane labor guidelines, zero forced overtime, standardized workplace safety, and ethical remuneration matching modern supply compliance demands.
Full certified alignment with REACH (EU), Prop 65 (California), and OEKO-TEX Standard 100 protocols. Zero heavy metals, hazardous azo colorants, toxic formaldehydes, or banned plasticizers.
Custom barcode labeling, localized inner carton drop testing (ISTA 1A), polybag warnings, and coordinated pallet delivery routing to Amazon FBA, DTC fulfillment hubs, or regional ports (FOB Qingdao, CIF, DDP).
Bilingual tech packs and real-time merchandiser liaison support. Speak directly with English-fluent project leaders who sit adjacent to our production lines, eliminating telephone communication gaps.
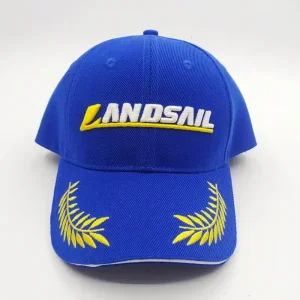
From upscale resort collections to extreme performance racing gear, our production lines construct bespoke hat profiles matched to market-specific tolerances.
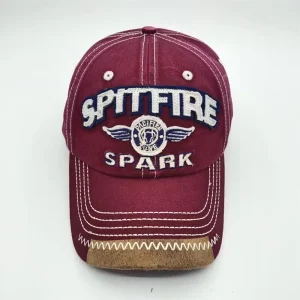
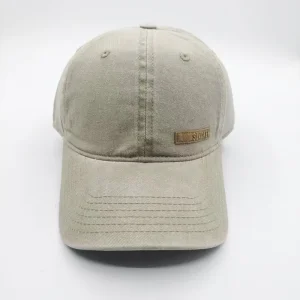
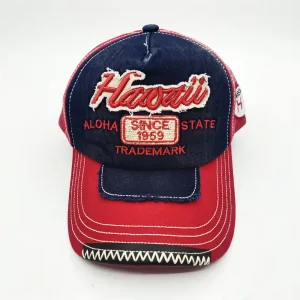
For independent brands demanding soft-washed vintage finishes, enzyme distressing, high-density 3D puff embroidery, and tactile woven trims. Minimalist 6-panel unconstructed silhouettes that align with contemporary urban trends.
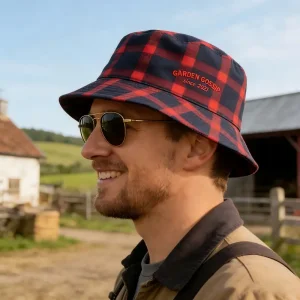
Reversible dual-patterned bucket hats, packable sun bonnets, and wide-brim silhouettes utilizing unbleached natural cotton canvas and organic linens. Complete with custom-branded detachable chin cords and anti-corrosive brass eyelets.
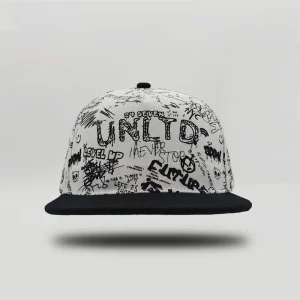
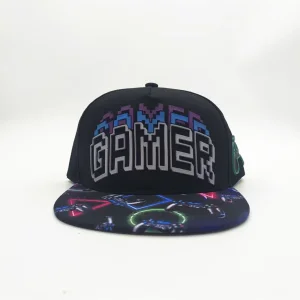
5-panel snapbacks and athletic caps customized for team supporters, tech brand pop-ups, and corporate giveaways. Formulated for rapid color-matching (Pantone PMS matching) with rubberized patch integration and gamer-centric details.
Driving smart manufacturing forward with digital sampling workflows, circular fibers, and responsive production algorithms.
Transitioning from traditional flat tech sheets to hyper-realistic CLO 3D virtual fittings. Brand owners can inspect pattern drape, curvature tensions, and thread density in high fidelity before physical needles touch textile, saving 40% in proto cycle time.
Advancing our procurement toward 100% ocean-bound recycled plastics (RPET), regenerated cellulose, and biodegradable plant-derived dye pigments that lower the chemical footprint per finished piece without compromising tensile durability or lightfastness.
Equipping our 5 sewing lines with semi-automated visual stitching stations and modular production cells. This allows Chenyou to sustain agile 100-piece runs while effortlessly scaling to 50,000+ units during seasonal peak waves without tool-retool bottlenecks.
Clear answers to standard commercial concerns regarding production capacities, sampling costs, trim choices, and logistical handoffs.
Our flexible MOQ starts at 100 pieces per style and colorway for custom embroidered baseball caps, trucker hats, and bucket hats. Emerging boutique labels can split colorways within a single silhouette to meet production criteria, lowering inventory risk.
Digital artwork and computerized embroidery tape digitizing are completed in 24–48 hours. Physical pre-production samples ship within 5–7 working days. Sample fees are universally deductible from initial bulk order deposits upon purchase confirmation.
We execute 3D puff embroidery, delicate flat chain-stitching, vintage appliqué, genuine & vegan leather patches, tactile PVC/silicone molded badges, screen and digital sublimation printing, custom metallic hardware, laser crown eyelets, and customized private interior seam tapes.
All caps undergo high-temperature industrial steam blocking followed by cardboard crown supports and custom double-wall corrugated export cartons. Every container is packed with humidity absorbers to avoid atmospheric moisture degradation throughout sea transit.
Engineered for international wholesale distributors, sports leagues, and lifestyle streetwear brand programs.