 Chenyou Hats Chenyou Hats
Explore our precision-crafted headwear collections engineered with premium materials, reinforced stitching, and advanced custom branding capabilities.
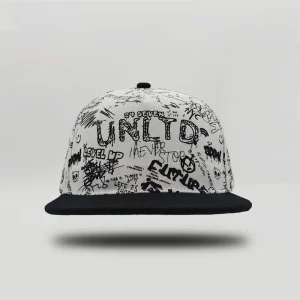
The global headwear landscape has undergone a tectonic shift. What was once considered a purely utilitarian cold-weather accessory has evolved into a strategic focal point for global fashion houses, outdoor technical wear outfitters, and corporate merchandise ecosystems. Modern procurement directors, brand founders, and global supply chain executives require a manufacturing partner capable of synthesizing advanced textile chemistry, rapid automated knitting technology, and seamless regulatory compliance.
The convergence of technical outdoor performance with urban streetwear ("Gorpcore") has amplified consumer demand for high-gauge Merino wool, moisture-wicking synthetic blends, and architectural rib-knit structures. Beanies must now perform seamlessly in sub-zero alpine conditions while maintaining structural aesthetics for metropolitan environments.
Enterprise buyers across North America and Europe face escalating regulatory scrutiny regarding material origin and carbon emissions. Sourcing certified GRS (Global Recycled Standard) polyester, OEKO-TEX Standard 100 non-toxic dyes, and organic GOTS cotton has shifted from an optional marketing bonus to an absolute procurement imperative.
Traditional supply chain models with 180-day lead times and multi-thousand minimum order quantities (MOQ) are failing modern direct-to-consumer (D2C) brands. Today’s market leaders leverage agile manufacturing clusters like Qingdao Chenyou to execute rapid prototyping within 7–10 days and roll out seasonal inventory in responsive micro-batches.
At Qingdao Chenyou Hat Industry Co., Ltd., we combine decades of craftsmanship with computer-controlled multi-gauge circular knitting equipment (WHOLEGARMENT® technology). The structural integrity, thermal retention rate (CLO value), and pilling resistance of a men's beanie are directly governed by yarn selection and machine gauge calibration.
| Yarn Type / Blend Composition | Thermal CLO Value | Moisture Vapor Transmission | Pilling Resistance (Grade 1-5) | Optimal Commercial Application |
|---|---|---|---|---|
| 100% Australian Merino Wool (19.5 Micron) | 0.85 High Thermal Retention | 940 g/m²/24h (Breathable) | Grade 4.0 (Anti-Pilling Finish) | Premium Alpine & Executive Luxury Collections |
| GRS Certified Recycled Acrylic (100%) | 0.72 Medium-High Retention | 620 g/m²/24h | Grade 4.5 (High Durability) | High-Volume Retail & Corporate Merchandise |
| 70% Acrylic / 30% Fine Wool Blend | 0.78 Balanced Warmth | 780 g/m²/24h | Grade 4.2 | Urban Streetwear & Daily Lifestyle Brands |
| Thermalite® Hollow-Fiber Polyamide | 0.91 Ultra-High Performance | 1,100 g/m²/24h (Fast Dry) | Grade 5.0 (Extreme Wear) | Tactical Gear, Winter Sports & Outdoor Workwear |
| Organic GOTS Cotton / Cashmere (85/15) | 0.65 Soft Mild Insulation | 890 g/m²/24h | Grade 3.8 | Spring/Autumn Transitional Lightweight Beanies |
Our automated manufacturing facility accommodates various machine gauge standards to suit your target brand positioning: 3GG Heavy Chunky Knit (for rugged, fisherman-style textured beanies), 7GG Standard Rib Knit (the classic versatile fold-over beanie density), and 12GG Fine Gauge Technical Knit (sleek, low-profile helmet liners and executive understated designs).
We offer comprehensive surface embellishment technologies engineered specifically for elastomeric knit textiles:
Precision-cut pattern designs that guarantee perfect ergonomic fit and retention across wear cycles:
Qingdao Chenyou Hat Industry Co., Ltd. represents the pinnacle of modern headwear production in Ligezhuang Town — widely recognized as China's global capital for headwear manufacturing. Founded in 2008 by industry pioneer Emma Wang following her intensive study of Japanese textile engineering in 1996, the enterprise has grown into a 5,000 square meter integrated manufacturing titan.
Situated in Ligezhuang Town, our facilities draw directly from localized raw material yarn spinning mills, custom dye houses, and specialized trim artisans. This hyper-dense industrial ecosystem reduces component lead times by up to 60% compared to isolated production facilities worldwide.
Inherited from Emma Wang's foundational experience in Japanese production units, our factory operates under rigorous 5S operational methodologies and strict AQL 1.5/2.5 inspection benchmarks. Every single beanie undergoes needle detection testing prior to final export packaging.
Housing 5 specialized assembly and knitting lines operated by over 100 skilled technicians, our plant delivers an annual capacity exceeding 3 million units while preserving the tactile craft quality demanded by luxury apparel brands.
Procurement directors require transparency, predictability, and risk mitigation. Our standardized 6-phase original equipment manufacturing (OEM) and original design manufacturing (ODM) protocol ensures seamless execution from conceptual tech-pack analysis to final DDP port delivery.
Our engineering team analyzes vector tech packs, specifies exact Pantone (PMS) color matches, and verifies structural feasibility within 24 hours.
Physical golden samples are produced on computerized sample machinery and dispatched via express courier for hands-on approval.
Raw materials undergo OEKO-TEX certified reactive dip-dyeing with color fastness testing to guarantee zero bleeding across wash cycles.
Multi-feed knitting machinery executes structural body panels, followed by manual top closure joining and trim application.
Navigating customs regulations, chemical safety bans, and ethical audit standardizations is vital for modern multinational importers. Qingdao Chenyou Hat Industry Co., Ltd. provides complete documentation packages ensuring total compliance across North American, European, Japanese, and Australian customs ports.
All raw yarns, thread materials, plasticizers, and dyes are independently tested to meet EU REACH Annex XVII standards and US CPSIA lead/phthalate limits, protecting your brand against safety recalls.
Our facilities undergo regular third-party social compliance audits (BSCI / WRAP / ISO9001), verifying fair wage practices, occupational health standards, and strictly zero child or forced labor usage.
We support FOB Qingdao, CIF, CFR, as well as full DDP (Delivered Duty Paid) door-to-door shipping solutions with import customs clearance handled directly by our global logistics network.
Headwear design must reflect the end-user's environmental realities and lifestyle aspirations. Our custom beanie configurations are engineered for distinct market verticals:
Targeted at ski apparel brands, mountaineering outfits, and winter sports retailers. Incorporating Thermalite® or Merino wool yarns, windproof internal fleece linings, reflective high-visibility yarns, and snug ergonomic skull-cap fits designed to be worn comfortably underneath technical helmets.
Designed for boutique fashion houses and trend-forward streetwear labels. Utilizing 100% fine Cashmere or extra-fine 19.5-micron Merino wool, custom-dyed seasonal palettes, subtle debossed metal or leather branding badges, and oversized slouchy or short docker silhouettes.
Engineered for large-scale corporate gifts, industrial workwear uniforms, and promotional merchandise programs. Focused on cost-effective GRS recycled acrylics, high-durability non-pilling yarns, and high-visibility 3D embroidered company logos with exceptional wash resilience.
Tailored for cold-weather marathon running, tactical training, and outdoor fitness brands. Featuring ultra-lightweight 12GG fine-gauge construction, mesh-knit breathability zones over sweat-prone areas, moisture-wicking synthetic yarn blends, and integrated ponytail or headphone pass-throughs.
Get definitive technical answers regarding custom beanie production, sampling lead times, material compliance, minimum order quantities, and custom packaging.
Our flexible manufacturing setup accommodates orders starting as low as 100 to 300 pieces per style/colorway for standard stock yarns (such as acrylic or cotton blends). For custom Pantone-dyed yarns or specialized technical fibers (such as 100% Australian Merino wool or Thermolite®), our standard MOQ is typically 500 pieces per colorway. We also offer prototype development runs for enterprise brands expanding new seasonal lines.
Standard sample development requires 7 to 10 business days after digital vector tech-pack confirmation. Mass production lead times generally range between 20 to 30 calendar days, depending on order volume, stitch complexity, and custom hardware embellishments. Rush production services can be negotiated for time-sensitive retail campaign deadlines.
Following Japanese-standard manufacturing protocols introduced by founder Emma Wang, we execute a rigorous 5-stage quality assurance process: raw yarn incoming tensile inspection, in-line knitting tension checking, linking/seam stress testing, post-wash dimensional stability audits, and 100% metal/needle detection passing prior to individual polybagging.
Yes. We offer fully certified sustainable options, including GRS (Global Recycled Standard) recycled polyester and acrylic made from post-consumer plastic bottles, GOTS certified organic cotton, and mulesing-free traceable Merino wool. Full chemical test documentation and transaction certificates (TC) can be supplied with shipments.
We provide complete OEM branding packages: custom woven main labels, satin care labels, hangtags with barcode/UPC sticker application, debossed leather or rubber patch sewing, 3D puff embroidery, custom tissue wrapping, and branded eco-friendly polybags or rigid presentation boxes ready for direct retail shelving.
Browse additional high-demand custom caps, beanies, and sun hats manufactured in our certified Qingdao facility.