 Chenyou Hats Chenyou Hats
Explore our premier engineered baseball caps, bucket hats, and custom winter headwear designed for international retailers and global brands.
Understanding the structural transition in global headwear sourcing: Eco-textiles, shade psychology, and ESG-driven procurement trends.
The global headwear market has undergone a fundamental transformation over the past decade. No longer viewed simply as utilitarian sportswear or casual merchandise, the baseball cap—and specifically the green baseball cap segment—has emerged as a focal point for fashion branding, corporate ESG (Environmental, Social, and Governance) identity, and technical textile engineering. Valued at over $18.4 billion globally in 2025, the headwear sector is experiencing an accelerated compound annual growth rate (CAGR) of 6.8%, with sustainable and specialized colorway sub-categories outperforming baseline growth at 8.7% annually.
From an industrial perspective, the color green in headwear manufacturing carries unique significance. Scientifically associated with sustainability, vitality, and organic authenticity, green headwear serves as a visual bridge between eco-conscious consumerism and premium aesthetic appeal. Global procurement managers from premier streetwear lines, professional sports franchises, and Fortune 500 corporate buyers are increasingly seeking specialized OEM/ODM manufacturers capable of delivering precise shade consistency (Pantone matching), eco-friendly low-impact dyeing, and superior structural longevity.
Global brand owners require GOTS-certified organic cotton, rPET (recycled polyester), and closed-loop waterless dyeing process compliance to align with corporate zero-carbon roadmaps.
Achieving uniform fastness across deep forest tones and pastel mint hues requires advanced spectrophotometer color matching and Delta-E < 0.8 tolerance standards.
Enterprise buyers are shifting away from fragmented trading agents, partnering directly with fully integrated Chinese manufacturing facilities offering rapid sample turnarounds within 7 days.
A detailed analysis of structural paneling, crown reinforcements, brim memory curved PE boards, and moisture management systems.
Creating a global leading green baseball cap demands strict adherence to textile engineering benchmarks. What separates a commercial-grade headwear item from an inferior promotional product lies in the technical formulation of fabric weight, seam density, visor memory retention, and inner sweatband construction.
Premium green caps utilize heavy-duty cotton twill (ranging from 260 GSM to 380 GSM), brushed canvas, or recycled technical polyester blends. The choice of weave dictates structural crown stability, breathability, and dye absorption depth:
Below is the benchmark standard enforced at Qingdao Chenyou Hat Industry Co., Ltd. for enterprise-level custom cap manufacturing:
| Component / Parameter | Standard Specification | Enterprise Performance Grade | Quality Verification Method |
|---|---|---|---|
| Crown Panel Stitching | 8 – 10 Stitches Per Inch (SPI) | High-Density Lockstitch | Visual Microscopic Inspection |
| Visor Insert Material | 100% Virgin High-Density PE Board | Shape Memory Bendable (1.8mm – 2.5mm) | Flexural Stress Resistance Test |
| Sweatband Construction | 4-Layer Moisture-Wicking Cotton/Poly | Anti-Bacterial Dry-Tech Lining | AATCC 195 Liquid Absorbency |
| Color Fastness (Green Dyes) | Grade 4.5+ (Light & Washing) | ISO 105-B02 / ISO 105-C06 Standard | Spectrophotometer & Xenon Arc Test |
| Buckle & Closure Hardware | Embossed Brass / Matte Alloy / Snapback | Anti-Rust Electroplated Surface | 48-Hour Salt Spray Corrosion Test |
| Logo Embroidery | 3D Puff / Flat High-Density Stitch | Japanese Tajima Automated Embroidery | Tension & Thread Count Audit |
Why global brands partner with Qingdao Chenyou Hat Industry Co., Ltd. for end-to-end OEM & ODM supply chain reliability.
In global headwear manufacturing, regional industrial clusters determine supply chain resilience, cost efficiency, and design innovation. Located in Ligezhuang Town, Jiaozhou City, Qingdao, China—world-renowned as the premier "Capital of Headwear Manufacturing"—Qingdao Chenyou Hat Industry Co., Ltd. sits at the heart of an unprecedented industrial supply ecosystem.
With over 18 years of specialized manufacturing experience, our 5,000+ square meter state-of-the-art facility integrates all stages of production—from raw textile selection and computerized laser cutting to high-precision Tajima embroidery, automated stitching, assembly, and multi-stage quality control.
Direct relationships with local yarn spinning mills and dye houses allow us to lock in volume pricing on custom Pantone green fabrics, reducing raw material lead times by up to 35% compared to non-clustered factories.
Deploying multi-head Tajima embroidery machines, automated eyelet punches, and ultrasonic brim-stitching equipment ensures stitch-level precision across tens of thousands of units with minimal human error.
Our specialized sample development workshop produces physical prototypes within 7 to 10 business days, allowing emerging fashion labels and corporate clients to validate designs rapidly without massive capital tie-ups.
Situated just 30 minutes from Qingdao Port (Qingdao Jiaodong International Airport & Deepwater Sea Port), we deliver seamless FOB, CIF, or DDP shipping solutions with real-time tracking to North America, Europe, Australia, and Asia.
How custom green baseball caps serve diverse market verticals—from high-fashion streetwear to corporate branding and outdoor apparel.
Vintage washed forest green "dad hats" and 6-panel unstructured caps featuring 3D puff embroidery, vintage brass strap closures, and distressed brims dominate modern urban apparel channels.
Enterprises utilizing green headwear crafted from GOTS organic cotton or rPET fabric to signal corporate commitment to environmental sustainability during tradeshows, staff uniforming, and campaigns.
Classic emerald green and sage caps engineered with moisture-wicking sweatbands, UV protection, and laser-perforated side ventilation panels tailored for elite golfers and resort pro shops.
Durable olive green and camouflage utility caps featuring quick-dry nylon, water-repellent DWR coatings, and packable visors designed for hiking, fishing, and adventure excursions.
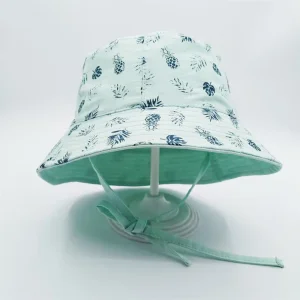
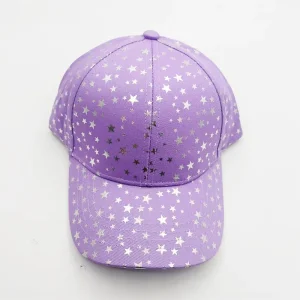
Light green leaf-printed and star-embellished caps using non-toxic, hypoallergenic dyes and soft-snap adjustable closures certified safe for kids aged 3 to 12 under international CPSIA standards.
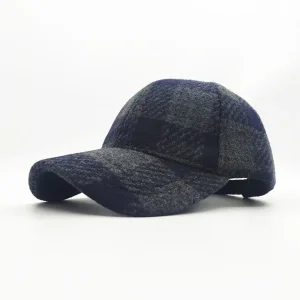
Heavyweight green plaid wool caps offering winter thermal warmth with structured vintage silhouettes, perfect for autumn/winter retail catalog rollouts in colder climates.
How technological convergence, smart textiles, and zero-impact manufacturing processes are revolutionizing baseball cap production.
As the global headwear industry progresses, purchasing directors must stay ahead of shifts in consumer expectations and technological innovation. The next generation of baseball cap manufacturing is defined by three main pillars:
Traditional dyeing processes consume vast volumes of water. Advanced factories are introducing Supercritical CO2 dyeing technology, achieving vibrant Pantone green saturation without liquid wastewater discharge.
Integrating micro NFC chips underneath embroidered sweatband labels allows brands to offer anti-counterfeiting verification, digital storytelling, and eco-traceability directly to end consumers via smartphone scan.
Replacing standard plastic visors with bio-based PLA (Polylactic Acid) visor inserts derived from sugarcane starch ensures that caps are fully recyclable and ocean-safe at the end of their lifecycle.
Essential compliance checklists for B2B buyers evaluating green baseball cap manufacturers.
When sourcing headwear at scale, international buyers must verify that manufacturing partners adhere to international quality management and social compliance standards. Qingdao Chenyou Hat Industry Co., Ltd. maintains rigorous factory audits to guarantee zero disruption in global supply chains:
Clear, expert answers regarding custom green baseball cap manufacturing, lead times, MOQ, and technical customization options.
Our standard production MOQ starts as low as 100 to 300 pieces per style/colorway for stock fabric shades. For custom-dyed Pantone green fabrics or bespoke eco-textiles (e.g., organic GOTS cotton), the recommended volume is 500 pieces per batch to optimize dye-lot efficiency.
We utilize X-Rite industrial spectrophotometers to measure dye lot lab dips against official Pantone TCX / PMS color swatches under D65 standard light boxes. We guarantee a strict color tolerance rating of Delta-E < 0.8 prior to bulk fabric cutting.
Physical sample turnaround takes 7 to 10 business days following digital artwork approval. Mass production lead time is typically 15 to 25 days depending on design complexity, logo embroidery density, and order volume.
Yes. We specialize in GRS-certified recycled polyester (rPET) made from ocean plastic bottles, GOTS-certified organic cotton, and unbleached natural canvas paired with non-toxic, eco-friendly green dye processes.
We offer 3D puff embroidery, flat high-density embroidery, woven patches, genuine leather or vegan PU patches, screen printing, rubberized TPU badges, metal logo plates, and printed inner seam taping.
We offer comprehensive shipping solutions including FOB Qingdao, CIF, CFR, and hassle-free DDP (Delivered Duty Paid) service via air express or sea freight directly to your warehouse, managing all customs paperwork and duty filings.
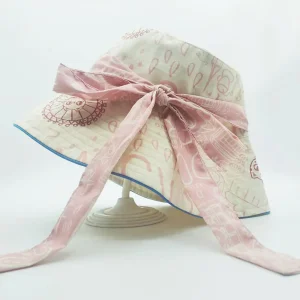
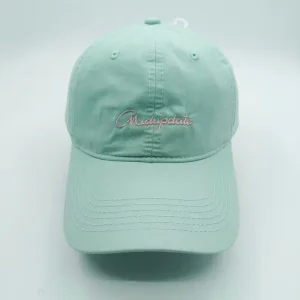
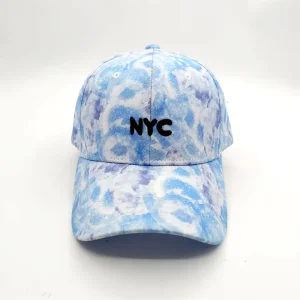
Discover more custom baseball caps, mint green embroidered summer hats, snapbacks, and reversible bucket caps available for OEM manufacturing.