 Chenyou Hats Chenyou Hats
Over the past five years, the global apparel landscape has witnessed a fundamental shift away from stark neon accents toward rich, organic earth tones. Among these, brown—spanning shades of mocha, espresso, chestnut, tobacco, and vintage washed khaki—has emerged as the dominant neutral anchor for modern streetwear labels, luxury athleisure, and outdoor lifestyle brands. B2B procurement data indicates a 142% year-over-year surge in demand for wholesale brown baseball caps. This aesthetic pivot reflects consumer desire for versatile, timeless accessories that harmonize with minimalist capsule wardrobes, workwear aesthetics, and vintage utility fashion.
For global distributors, retail chain buyers, and private label e-commerce merchants, stocking premium brown headwear yields significantly higher sell-through rates compared to seasonal trend colors. Earth-tone baseball caps maintain multi-season viability, spanning Spring/Summer sun protection and Autumn/Winter wool-blend layering. By sourcing directly from specialized OEM/ODM factories, wholesale buyers achieve optimal cost-per-unit metrics, unlocking gross margins exceeding 65–75% when retailed in North American, European, and Asia-Pacific consumer markets.
Established in 2008, Qingdao Chenyou Hat Industry Co., Ltd. operates a modern 5,000 square meter manufacturing plant equipped with 5 automated sewing lines and over 100 highly skilled technicians. Our strategic location in Ligezhuang Town grants direct access to specialized raw material markets, high-precision embroidery suppliers, and the deepwater shipping facilities of Qingdao Port, ensuring seamless global logistics.
From initial sketch digitizing and rapid 3D prototyping to mass cutting, embroidery, structured panel fusing, and final steam shaping, we offer complete turn-key solutions. Brands can fully customize crown structures (6-panel, 5-panel, unstructured dad cap), visor curves, closure buckles, sweatband cushioning, and interior seam taping.
Quality failure is not an option for international retail brands. Our factory enforces a rigorous 6-stage QC protocol: fabric pull-strength verification, color-fastness lab testing, pattern-matching inspection, embroidery density validation, crown symmetry check, and metal detector needle inspection prior to automated carton packing.
| Specification Parameter | Standard Wholesale Specs | Premium Enterprise Specs | Technical Functionality |
|---|---|---|---|
| Primary Fabric | 100% Chino Cotton Twill (260 GSM) | Heavyweight Heavy Cotton Twill / Stretch Suede / Corduroy (320–380 GSM) | Enhanced structural longevity, soft hand-feel, rich texture depth for brown tones. |
| Crown Construction | 6-Panel Unstructured "Dad Cap" | 6-Panel Structured with Hard Buckram Fusing / 5-Panel High Crown | Maintains crisp silhouette, prevents forehead sagging under heavy embroidery. |
| Sweatband & Interior | Standard 100% Cotton Taping | 4-Layer Moisture-Wicking Performance Foam + Antimicrobial Mesh | Absorbs sweat, reduces friction, enhances comfort for extended wear. |
| Logo Branding Options | Flat 2D Thread Embroidery | High-Density 3D Puff Embroidery / Embossed Genuine Leather Patch / Metal Badge | Delivers high visual contrast against dark mocha and light tan cotton substrates. |
| Color Fastness Standard | Grade 3.5 (AATCC Standard) | Grade 4.0–4.5 (ISO 105-B02 UV Light Exposure Certified) | Prevents color fading under intense sunlight, sweat accumulation, or gentle washing. |
| Closure Hardware | Plastic Snapback / Standard Metal Slide | Antique Brass Buckle + Tuck-in Leather Strap / Magnetic Speed Closure | Adds premium tactile value and vintage authenticity to brown headwear. |
Utilizing state-of-the-art multi-head Tajima and Barudan embroidery machinery, our factory executes intricate design details with thread counts up to 12,000 stitches per design. For brown baseball caps, popular embellishments include laser-engraved brown leather patches, woven damask labels, and raised 3D foam embroidery using contrast threads such as cream, gold, forest green, or matte black.
To achieve authentic vintage, retro, or heritage workwear finishes, we offer specialized post-assembly washing processes. Options include stone-washing, enzyme washing, acid-wash distressing, and localized brim abrasion. Our eco-friendly washing facilities strictly recycle process water while delivering uniform distressed aesthetics across thousands of production units.
All textiles, dyes, inner stiffeners, and metal hardware strictly adhere to EU REACH Regulation (EC No 1907/2006). Our brown fabric dyes are 100% Azo-free and free from heavy metals, formaldehyde, and phthalates, ensuring complete safety for direct skin contact.
Our supply chain partners are certified under OEKO-TEX Standard 100 Class I & II. This certifies that every component—from the sewing thread to the sweatband foam—has been tested for harmful substances, satisfying the demands of premium international retailers.
Qingdao Chenyou upholds fair labor practices, safe working environments, equal remuneration, and strict prohibition of child labor. Our factory facilities regularly pass BSCI and SEDEX SMETA 4-Pillar social audits, empowering enterprise clients to satisfy ESG compliance standards.
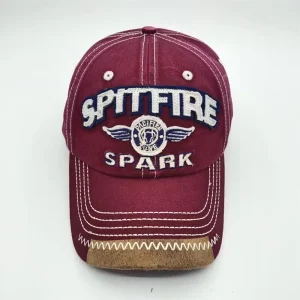
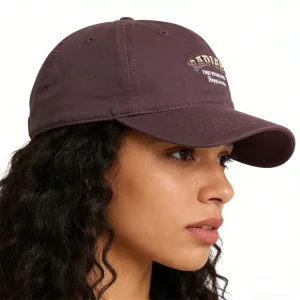
Distressed brown dad hats paired with minimal script embroidery or retro collegiate letters. Highly popular among Gen Z and millennial demographics seeking casual, vintage aesthetic headwear.
Earth-toned 5-panel trucker hats and canvas baseball caps engineered for hiking, fishing, and outdoor exploration. Earthy brown shades camouflage dirt while blending seamlessly into natural environments.
Heavy-duty duck canvas baseball caps with reinforced stitching and leather logo patches. Built for rugged durability, targeting tradespeople, craft breweries, and heritage fashion enthusiasts.
Premium custom-branded brown caps used as executive corporate gifts, employee uniforms, and promotional merchandise for specialty coffee roasters, automotive clubs, and tech firms.
Transitioning from virgin cotton to GRS-certified (Global Recycled Standard) recycled polyester and organic cotton blends. Sustainable brown dyes derived from upcycled plant matter and agricultural waste are reducing carbon footprints by up to 35%.
Deploying AI algorithms for digital marker laying and automated laser nesting. This technology maximizes fabric yield, reduces textile waste to less than 3%, and ensures micro-accurate panel matching across mass bulk order runs.
Embedding flexible, washable Near Field Communication (NFC) chips under sweatbands or inside visor seams. This empowers retail brands to offer digital authentication, exclusive content access, and supply chain transparency directly to end consumers.