 Chenyou Hats Chenyou Hats
Explore our primary manufacturing lines engineered for global distributors, fashion labels, and athletic franchises.
Why the red baseball cap remains an enduring high-conversion asset in global retail, corporate branding, and sports merchandising ecosystems.
The global headwear market has undergone a dramatic transformation over the past decade, evolving from a functional sun-protection category into a multi-billion-dollar global branding medium. Within this expansive sector, the wholesale global red baseball cap occupies a uniquely powerful position. Red is not merely a color choice; it is a high-visibility psychological driver that commands immediate visual dominance in sports arenas, retail environments, motorsport paddocks, and political campaigns.
From a commercial procurement standpoint, red baseball caps consistently deliver higher sell-through rates across North America, Western Europe, and the Asia-Pacific region. Market analysis indicates that corporate promotional buyers, athletic apparel sourcing managers, and high-street fashion labels allocate significant percentages of their annual headwear budgets specifically to red colorways (ranging from classic Pantone 186 C Crimson to Pantone 200 C Scarlet and deep Crimson Burgundy).
Red triggers high physiological arousal, increasing visual recall rates by up to 34% compared to neutral tones. It serves as the primary corporate color for automotive racing teams, energy beverage brands, and premium tech enterprises.
Projected to expand at a 6.4% Compound Annual Growth Rate (CAGR). Custom branded headwear demand is accelerating due to direct-to-consumer (DTC) apparel brand explosion and e-sports sponsorships.
Global procurement managers are shifting away from generic stock caps toward deep OEM custom-dyed fabrics, custom structured crowns, and anti-fade UV-treated color formulas to maintain brand consistency.
Understanding yarn count, weave density, color fastness ratings, and structural buckram engineering in premium red cap manufacturing.
A red baseball cap appears simple on the surface, but engineering a cap that retains its structural integrity and vibrant hue under heavy sunlight, sweat exposure, and machine laundering requires rigorous textile engineering. As a leading manufacturer based in Qingdao, China, Qingdao Chenyou Hat Industry Co., Ltd. implements industrial-grade quality parameters for every raw material specification.
| Material Category | Fabric Composition & Specs | Color Fastness Rating | Primary Industrial Application |
|---|---|---|---|
| Heavyweight Cotton Twill | 108x56 Thread Count / 280–320 GSM / 100% Combed Cotton | AATCC Grade 4.5 (Reactive Dyeing) | Premium Streetwear, Heritage Brands, Retail Fashion |
| Performance Polyester Mesh | 100% Breathable Micro-Mesh / 160 GSM / Moisture Wicking | ISO 105-B02 Grade 5.0 (UV Resistant) | Motorsports, Trucker Caps, Outdoor Athletics |
| Eco-Friendly rPET Fiber | Recycled Post-Consumer Poly / GRS 4.0 Certified / 240 GSM | AATCC Grade 4.0 (Eco Reactive Dye) | Sustainable Brand Merchandising, Corporate ESG Initiatives |
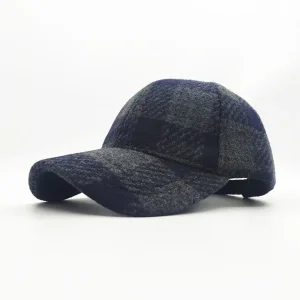
| Tweed & Wool Blends | 50% Wool / 50% Polyester Tartan Weave / 380 GSM | Dry Clean Fastness Grade 4.5 | Autumn/Winter Outdoor Lines, Vintage Racing Collections |
For structured 6-panel caps, we utilize fused double-layer resin buckram inside the front panels. This prevents front-panel collapsing while maintaining soft touch comfort against the wearer's forehead.
Our visors feature shape-memory virgin Polyethylene (PE) board inserts, available in pre-curved or flat profiles. They endure 180-degree flex testing without warping or snapping.
Multi-layer sweatbands with quick-drying foam padding and anti-bacterial weave inserts absorb moisture rapidly, preventing salt-stain ring formation on red exterior fabrics.
Why Qingdao / Ligezhuang Town represents the global pinnacle of custom headwear manufacturing throughput, precision, and cost efficiency.
Located in Ligezhuang Town, Qingdao—internationally recognized as the "Capital of Hat Manufacturing"—Qingdao Chenyou Hat Industry Co., Ltd. leverages an unmatched localized industrial ecosystem. Within a 10-kilometer radius, our operations are supported by specialized yarn spinning mills, custom buckle dye houses, high-precision embroidery digitized pattern makers, and logistics hubs connected directly to Qingdao Port.
This geographic concentration translates into unprecedented production speed, drastic reduction in raw material lead times, and substantial cost savings passed directly to international B2B buyers.
Equipped with 15-needle Japanese Tajima multi-head embroidery machines. We execute 3D Puff Embroidery, metallic thread stitching, intricate micro-patches, and chenille appliqués at 1,200 stitches per minute with zero thread breakage.
Our in-house design studio turns flat vector tech packs into physical prototype samples within 5 to 7 business days. We provide digital 3D rendering pre-approvals to expedite bulk production sign-offs.
Every manufacturing stage—fabric stress testing, panel cutting, embroidery alignment, crown blocking, needle detection, and final packing—undergoes rigorous AQL 1.5/4.0 inspection protocols.
A step-by-step operational roadmap for international buyers, sourcing agents, and brand managers.
Client submits artwork vectors (AI, EPS, PDF), desired Pantone codes (e.g., Pantone 18-1662 TPX Flame Scarlet), closure types (metal buckle, snapback, leather strap), and target target quantities.
We perform lab dip color matching and produce physical prototype caps. Embroidery digitized files are calibrated for stitch density and 3D height. Express courier dispatch in 7 days.
Upon PP sample approval and deposit confirmation, bulk manufacturing commences. Clients receive real-time production milestone updates via our digital MES tracking interface.
100% metal/needle detection and final AQL audit. Goods are custom cartons packaged, sea/air freighted under FOB Qingdao, CIF, or DDP terms directly to your distribution centers worldwide.
How red baseball caps are positioned across diverse consumer segments, regional markets, and industrial applications.
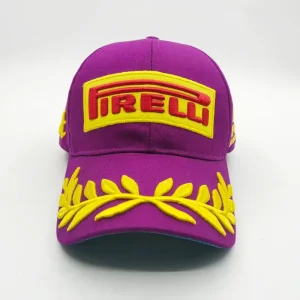
In Formula and GT racing circuits, red caps represent championship speed and legacy. Sourcing specifications emphasize 3D front championship crest embroidery, side sponsor patch integration, and breathable sandwich brim accents.
Washed cotton twill "Dad Caps" in crimson, burgundy, and brick red dominate metropolitan retail markets across Tokyo, London, and New York. Features un-structured low profiles, brass tri-glide sliders, and subtle vintage script stitching.
For high-impact promotional campaigns, large-scale events, and political rallies, high-volume production efficiency is critical. We deliver 5-panel structured polyester caps with transfer or screen-printed logos at high cost efficiency.
Innovations shaping the next decade of sustainable, tech-integrated, and highly custom headwear supply chains.
Supercritical CO2 waterless dyeing technology reduces chemical effluent by 98% while deepening color saturation in synthetic fibers, supporting EU environmental import mandates.
Embedded passive NFC micro-chips inside cap sweatbands allow premium streetwear brands to verify product authenticity instantly via smartphone scan, protecting brand equity.
Micro-encapsulated phase-change material (PCM) inner linings actively absorb head heat, stabilizing skin temperature during extreme outdoor sports activity.
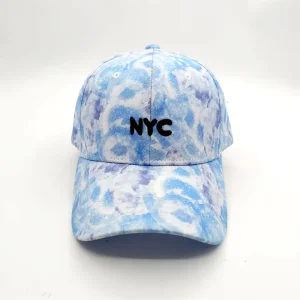
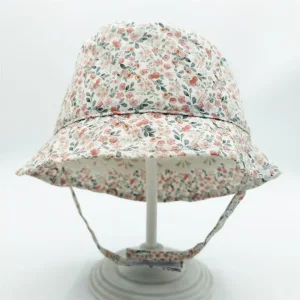
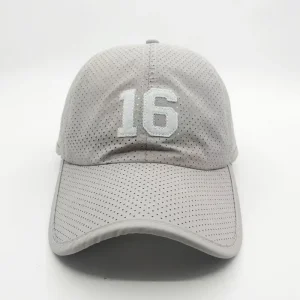
Explore additional specialized lines, including tie-dye finishes, children’s headwear, sports team editions, and casual caps.
Direct authoritative answers from Qingdao Chenyou’s senior engineering and export management team.
Take advantage of our 18+ years of OEM/ODM expertise, factory-direct pricing, fast 7-day sampling, and global logistics support. Request your custom quote and digital proof today.
Request Bulk Quotation & Technical Spec Sheet